Die casting at the core, coordinated end to end—an executable production plan your buyers can run.
Tooling starts only after mold sign-off. Mutual gain, shared success.
Three value pillars
Solution partner: die-casting core + coordination, plans you can run.
Die-casting core
High-pressure die casting for airtight and structural parts, controlled in one shot.
Up/downstream coordination
Machining, polish, surface, pack in one chain—release authority stays in-house.
Executable optimal plan
A production path built for your product landing—not a vanity brochure.
Process loop
Outsource is controllable; release stays in-house · see Quality
Machine→
Polish→
Surface outsource→
Return QC→
Pack
Case stories
Problem → method → result; figures from engineer source. More on Products.
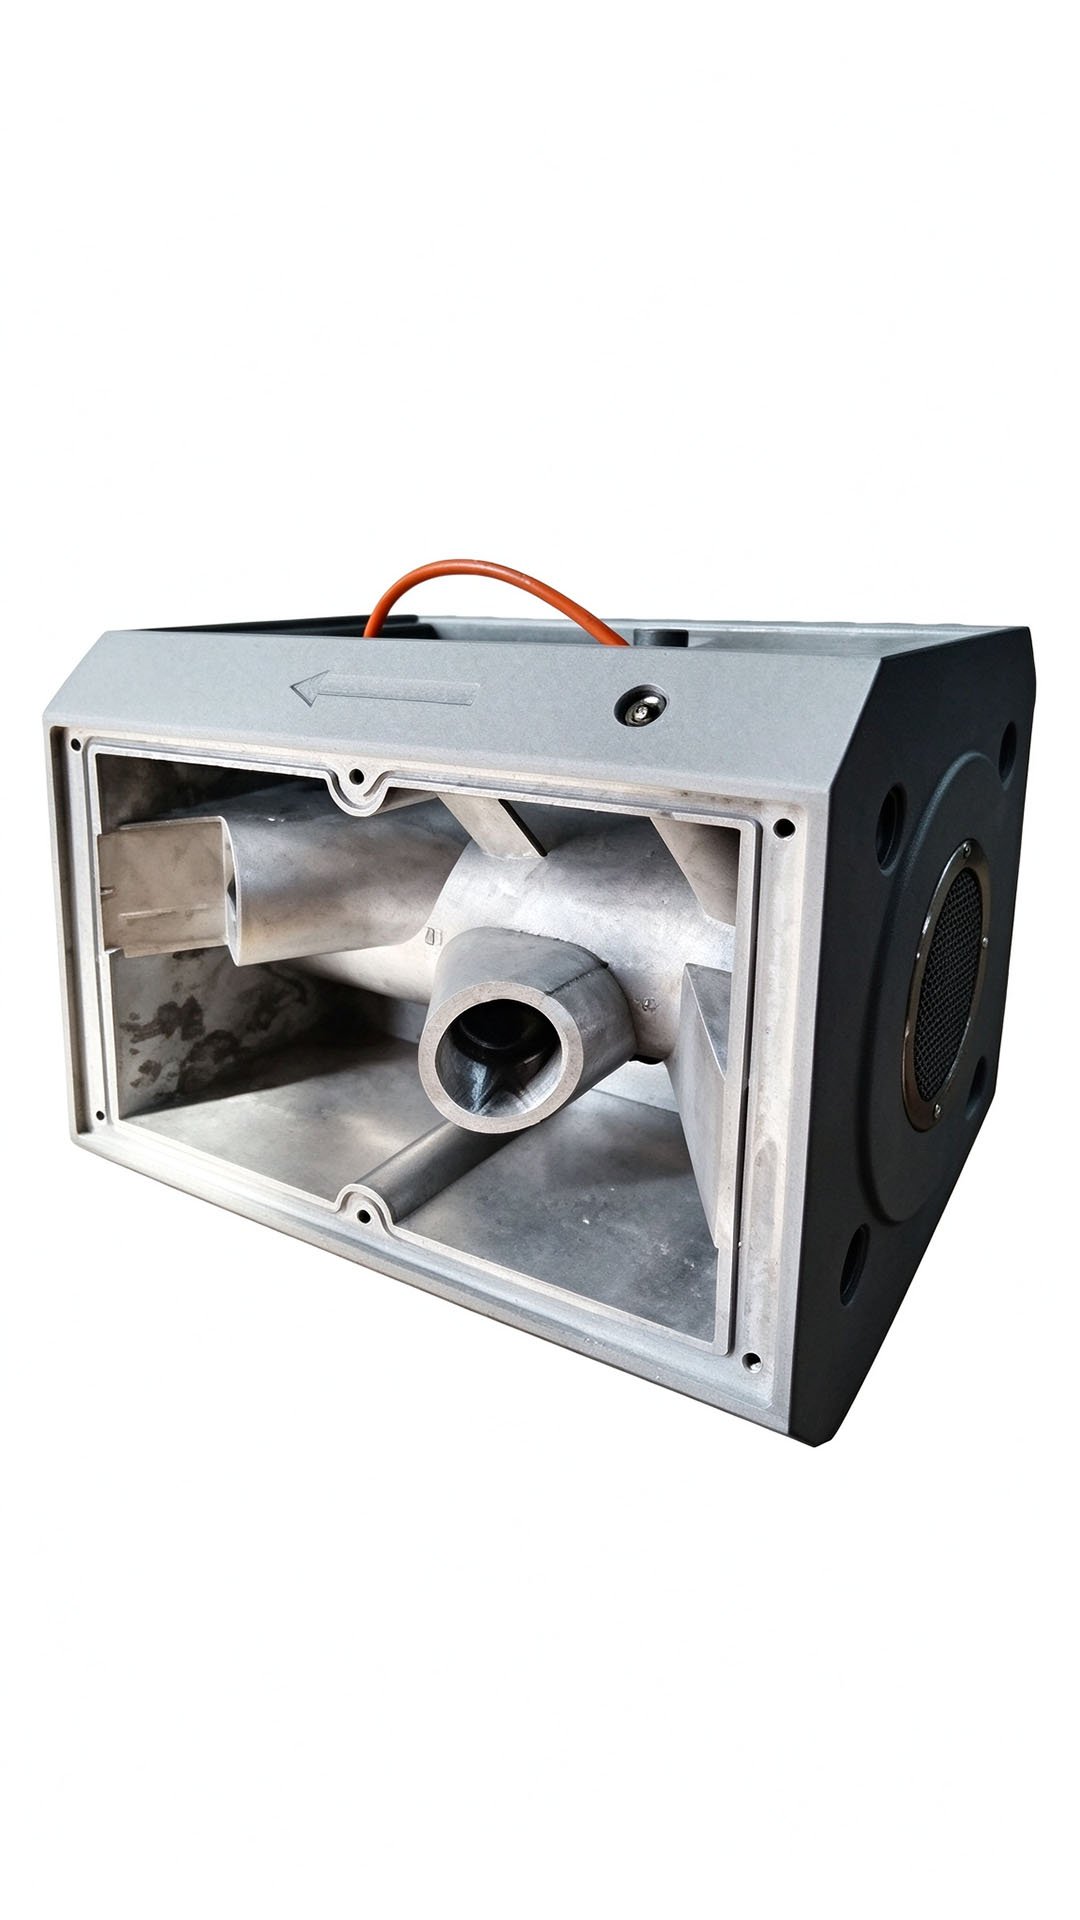
High-pressure die cast for airtightness—about 40% the cost of low-pressure
High-pressure die casting holds airtightness at roughly 40% of low-pressure cost. Vendors machine only; release stays in-house. Impregnation + pressure hold. Zero customer complaints after delivery.
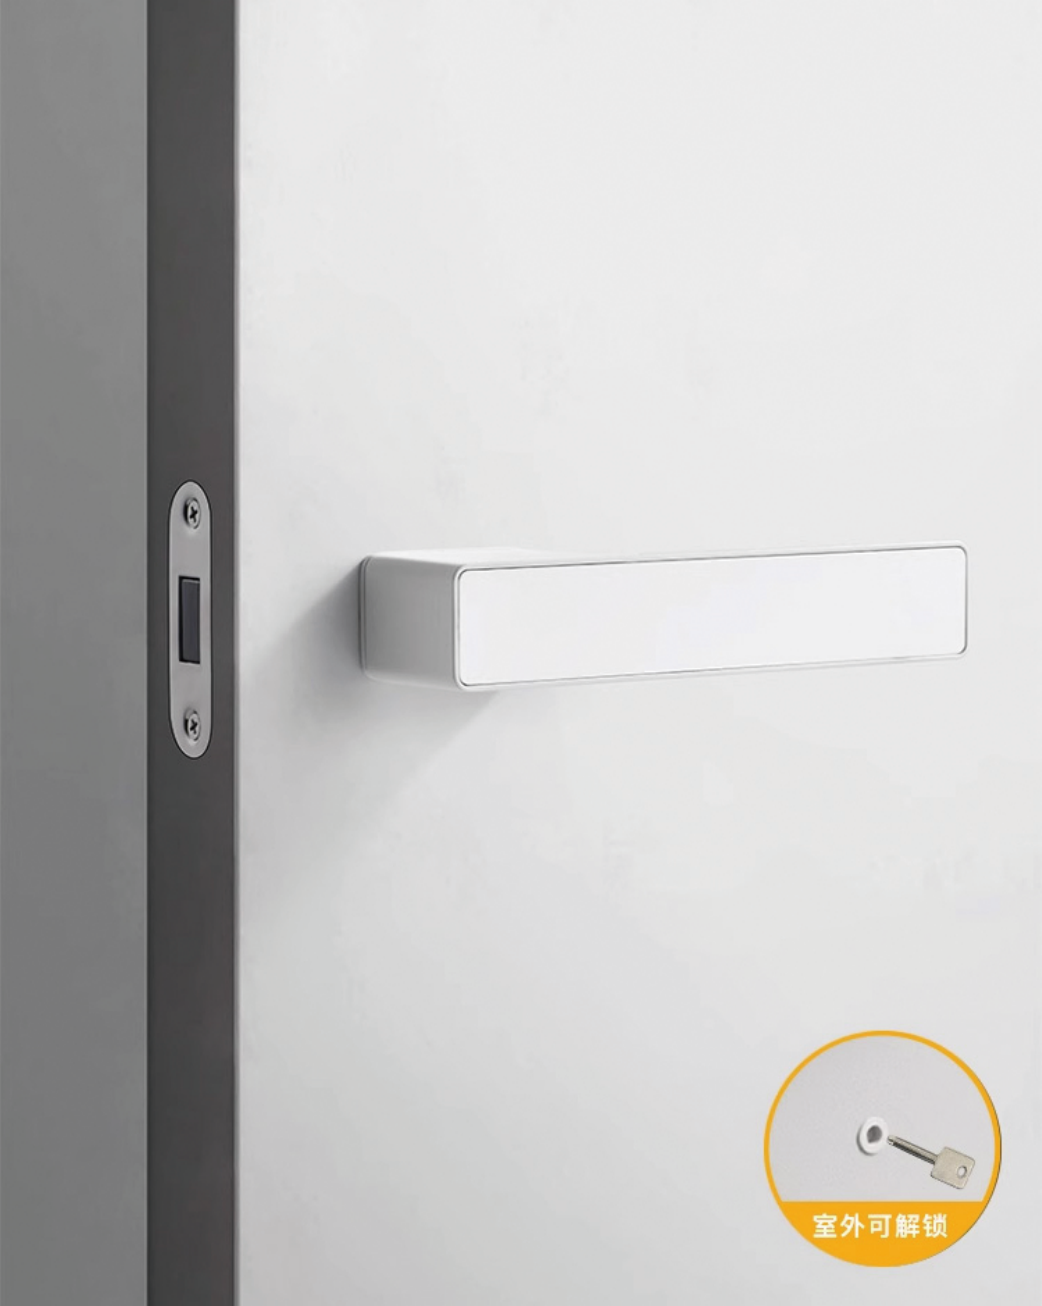
~40 material types into a finished lock—QC closed loop to ship
Nearly 40 material types assembled into a finished lock. Incoming → in-process → pre- and post-plating dual full inspection → outbound, one closed loop.
Plant trust bar
Facts only; mark TBD where visuals are missing.
~3,000 m²
EIA in place
Die cast → machine → polish → surface outsource → return QC → pack
16 polishing stations
8 polishers
~3,000 pcs/day plating-prep polish
~5,000 pcs/day paint-prep polish
equipment photos: TBD
Polish paths: plating-prep coarse→fine→hemp/cloth wheel; paint-prep coarse→fine→nylon wheel; 100% polish QC before ship.
Working principles
Mutual benefit, shared success
Long-term work follows executable plans—not empty slogans.
Mold confirmed before tooling kickoff
Drawings and mold sign-off first, then tooling and volume path.